

Rope Fastening Solutions for High-Rise and Heavy-Duty Elevators
As buildings continue to reach new heights, elevator systems must be designed to handle increased loads, longer travel distances, and more demanding operating conditions. In these environments, the performance of the elevator rope fastening system becomes even more critical.
High-rise elevators typically use longer steel wire ropes, which means that the total load carried by the rope fastening system is significantly higher. This requires fastening devices with greater strength and durability.
Heavy-duty elevators, such as freight elevators, also place higher demands on rope fastening systems. These systems must handle large and often uneven loads while maintaining reliable performance over time.
To meet these challenges, manufacturers design high-strength rope fastening solutions using advanced materials and reinforced structures. Alloy steel with enhanced mechanical properties is commonly used to ensure that the fastening device can withstand extreme loads.
In high-rise applications, resin socket systems are often preferred due to their superior load-bearing capacity and stability. These systems provide a strong and permanent connection that is well-suited for demanding conditions.
Engineers also consider factors such as rope elongation and load distribution. Proper design ensures that all ropes share the load evenly, reducing stress on individual fastening points.
Installation precision becomes even more important in high-rise systems. Small alignment errors can have significant effects over long distances, making accurate installation essential.
Advanced monitoring technologies are increasingly used in modern elevator systems. Sensors can detect changes in load, vibration, or temperature, allowing maintenance teams to monitor the condition of the rope fastening system in real time.
Regular maintenance is also critical in high-rise and heavy-duty applications. Due to the increased stress on components, more frequent inspections may be required to ensure continued safety.
As urban development continues to drive the demand for taller buildings and more powerful elevators, rope fastening systems will continue to evolve. Manufacturers are constantly improving designs to meet these growing challenges.
In these demanding environments, a reliable rope fastening system is not just a component—it is a fundamental requirement for safe and efficient elevator operation.
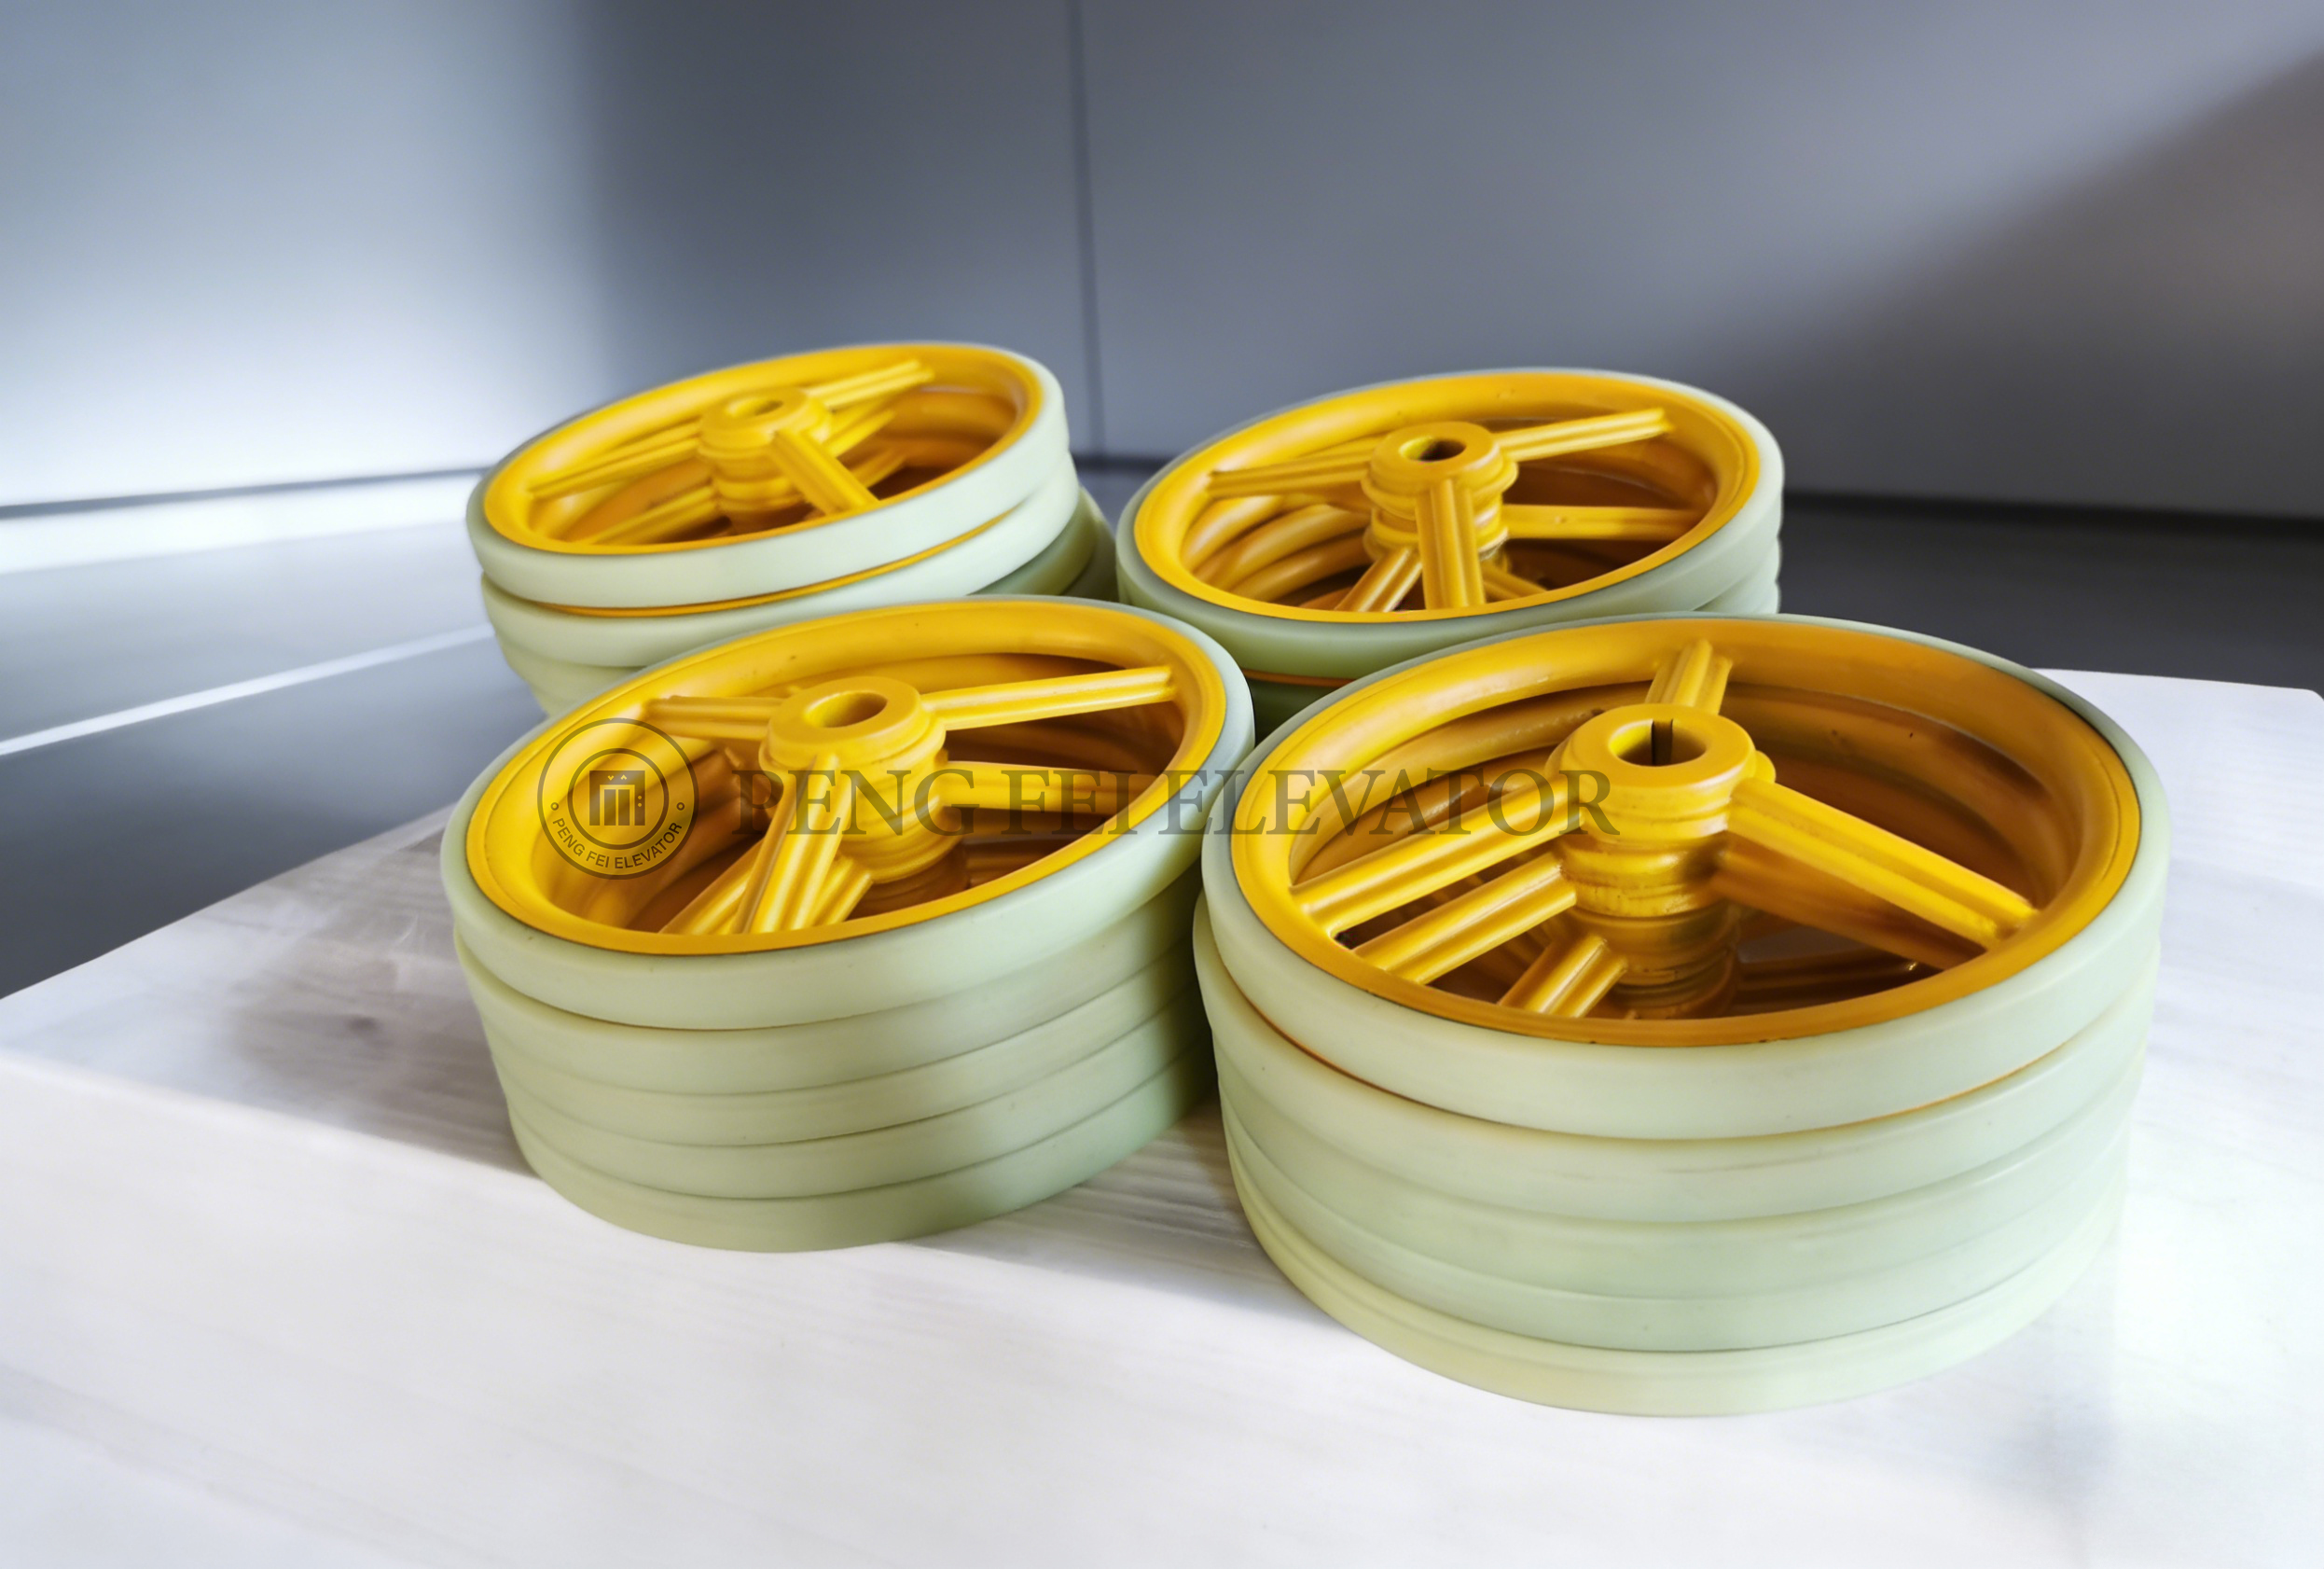
We offer various mechanical replacement parts for escalators and elevators. The products include escalator tooth plates, step frame strips, wear-resistant guide rail strips, step rollers, sprockets, driving rollers, driving friction wheels, driving shafts, gear assemblies, step chains, complete chain components, handrail belts, etc. In addition, we also provide elevator wire rope head assemblies, traction machine shock absorbers, car shock absorbers, sliding guide shoes, hollow guide rails, cast iron guide shoe shoes, traction wheels, guide wheels, buffers, etc. All wear-prone components suitable for electric escalators are compatible with mainstream elevator brands and are applicable for equipment maintenance, renovation projects, and new machine assembly. We offer OEM customization services and can handle large-scale orders as well as small-scale repair orders. Our products are of stable quality and the factory direct sales price has a significant advantage.